- Home
- About Us
- Products
- Knowledge
- Service
- Resource
- News
- Contact Us
Leave Your Message
In today's fast-moving industrial world, the importance of having precise and efficient fluid management systems really can’t be overstated. Sampling valves, for example, are super important—they help make sure that processes in industries like pharmaceuticals and food production stay on point and produce high-quality results. I read somewhere that, according to MarketsandMarkets, the global market for sampling valves is expected to see pretty significant growth. That’s mainly because more and more businesses are looking for reliable ways to control quality and make their processes smoother. Here at Wenzhou Lifei Stainless Steel Co., Ltd., we’ve been doing this for over 15 years, with a solid 13 years dedicated to exporting. We're passionate about creating innovative solutions that really fit our customers’ needs. Our goal is to help clients get the most out of sampling valves because we genuinely believe that their success is our success—and honestly, seeing our clients happy and satisfied keeps us going!
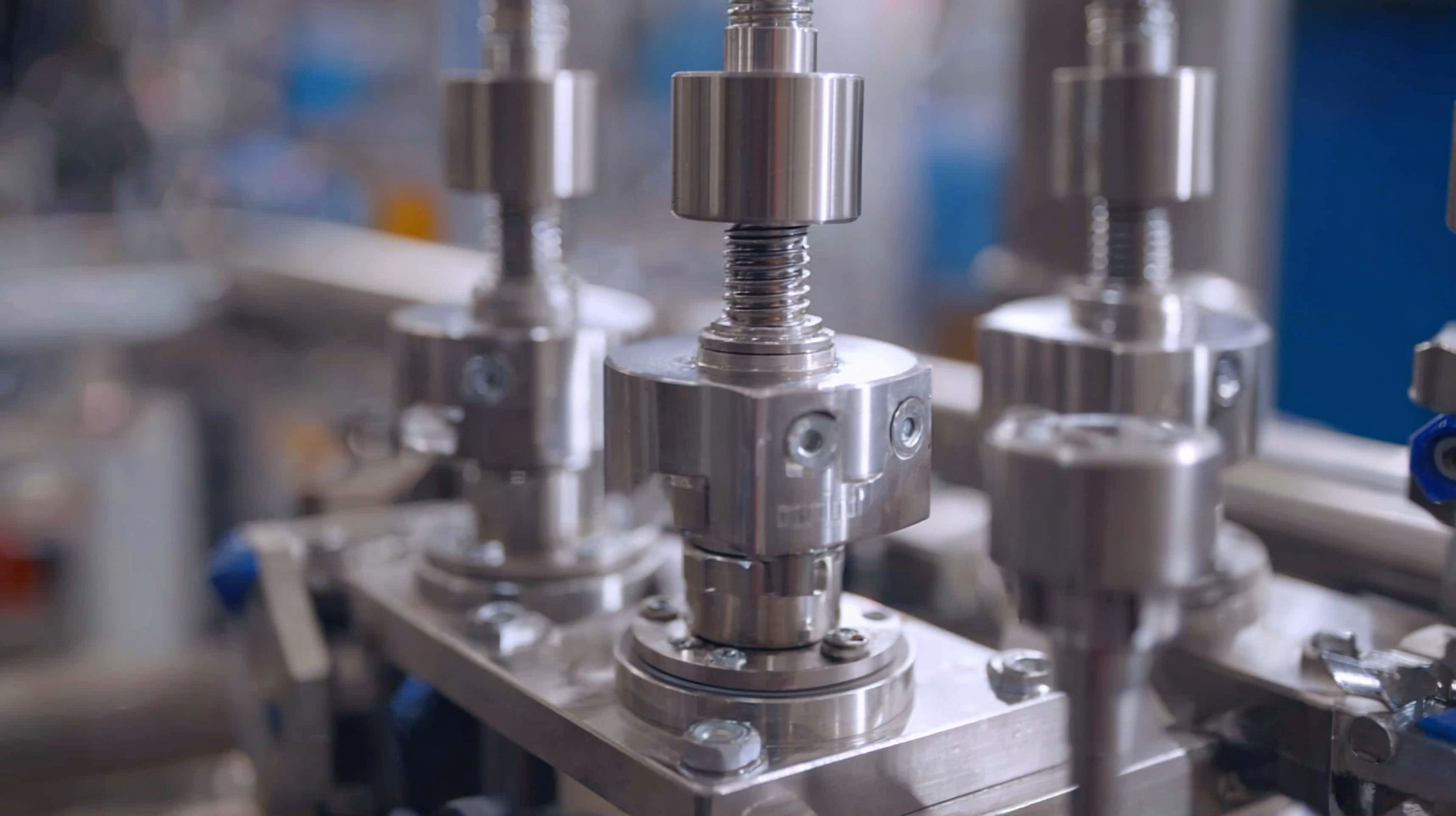
Sampling valves might not be the most glamorous piece of equipment, but they really play a vital role in keeping quality control in check across a bunch of different industries. Basically, they let you safely and quickly take fluid samples for testing—something that’s super important if you want to make sure your products meet quality standards and industry regulations. Did you know that, according to the International Society for Pharmaceutical Engineering, about 15% of failures in pharma manufacturing are linked to poor sampling practices? Yikes! That’s why using top-notch sampling valves can make a huge difference—helping to cut down on contamination risks and making sure the fluid’s characteristics are accurately represented.
At Wenzhou Lifei Stainless Steel Co., Ltd., we get how crucial reliable sampling solutions are. With over 15 years of experience in making fluid equipment, we always aim to put our customers first — offering innovative, efficient, and safe products. Using good quality sampling valves doesn’t just improve operational efficiency; it also helps companies hit higher marks when it comes to regulatory compliance. In fact, a report from the American Society of Mechanical Engineers shows that industries that stick to standardized sampling valves see up to a 20% bump in their compliance audit scores. We’re proud of our commitment to quality and customer satisfaction, and we’re confident our specialized solutions can really support your quality control efforts in a big way.
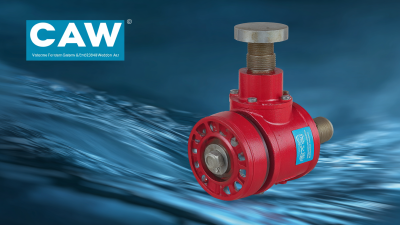
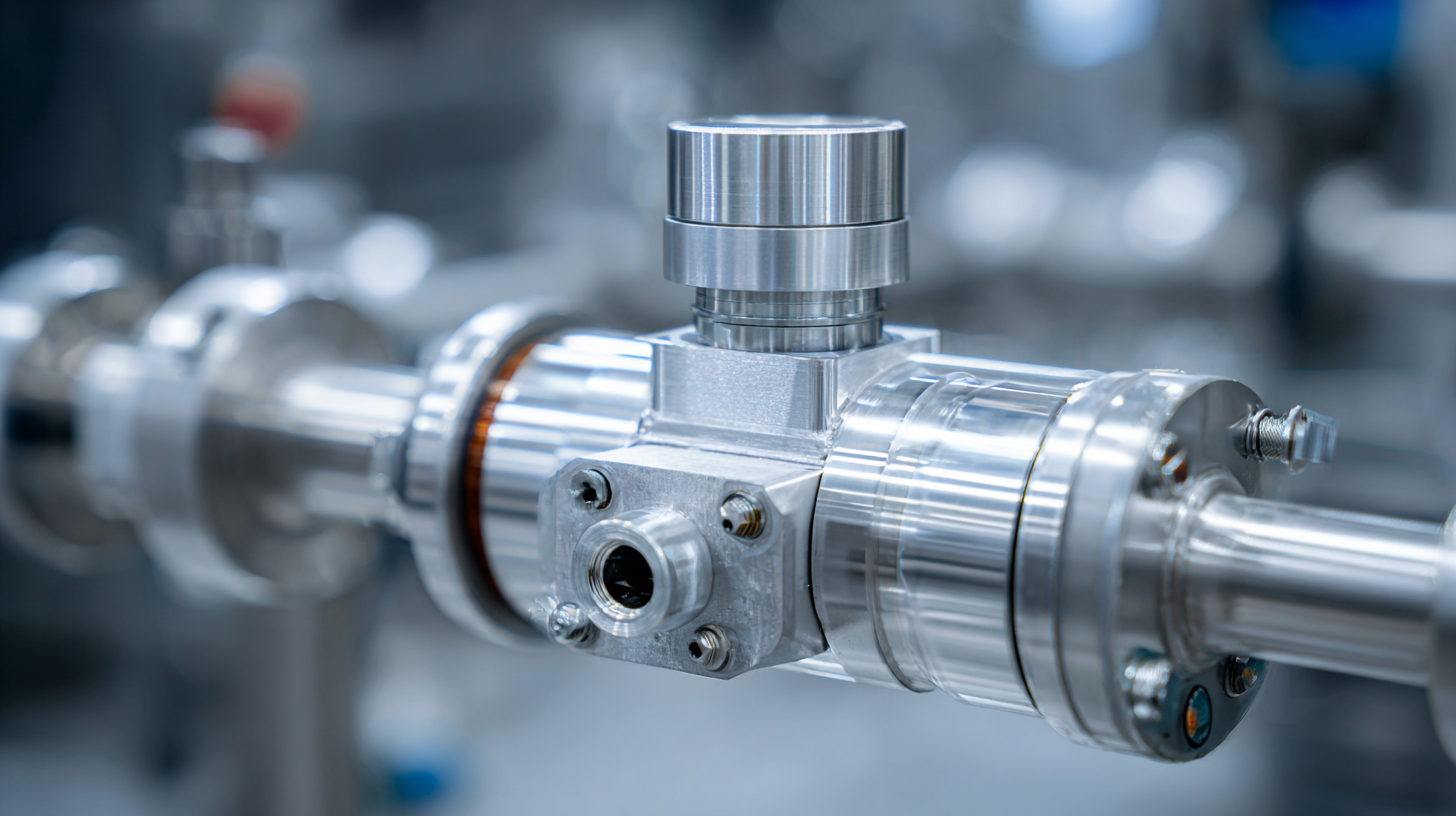
In today's fast-paced industrial environment, maintaining hygiene and operational efficiency is crucial, especially in sectors dealing with sensitive products. The LVM Stainless Steel Sanitary Aseptic Sampling Valves are designed specifically to meet these demands, offering a reliable solution for sampling medium-viscosity products. With the capability to handle viscosities ranging from 0 to 1,000 centipoise (cP) and particles up to 3mm in diameter, these valves are ideal for a diverse array of applications, including unprocessed milk, medical solutions, and various personal care products.
One of the standout features of LVM sterile sampling valves is their precision engineering, which ensures that hygiene standards are consistently met. The aseptic design minimizes the risk of contamination, making it particularly beneficial for industries where product integrity is paramount. Whether it’s filtered or unfiltered beer, creams, lotions, or perfumes, these valves are expertly calibrated to facilitate seamless sampling. This not only enhances operational efficiency but also streamlines quality control processes, allowing businesses to focus on innovation and production without compromising on safety or hygiene.
Choosing LVM Stainless Steel Sanitary Aseptic Sampling Valves is an investment in quality and reliability. By incorporating these valves into your production line, you can enhance not only the safety and cleanliness of your operations but also the overall effectiveness in managing product sampling across various industries.
: Sampling valves are essential for safely and efficiently collecting fluid samples for analysis, which is crucial for maintaining product quality and ensuring compliance with industry standards.
High-quality sampling valves can significantly reduce the risk of contamination and ensure accurate representation of fluid characteristics, which ultimately enhances operational efficiency and regulatory compliance.
Industries that utilize standardized sampling valves can experience up to a 20% improvement in compliance audit scores, helping to meet regulatory requirements more effectively.
Sampling valves allow for precise fluid sampling without full system interruption, conserving time and reducing the amount of raw materials wasted during testing, which is vital in sectors like pharmaceuticals and food processing.
By enabling accurate testing of small fluid volumes, sampling valves facilitate real-time quality assessments, allowing companies to quickly identify and address any deviations in product quality.
In the oil and gas sector, sampling valves help in monitoring fluid properties, improving operational efficiency, reducing costs by up to 15%, and enhancing safety while minimizing environmental risks.
Effective sampling systems using sampling valves can decrease the risk of spills and leaks during the sampling process, which is vital for complying with environmental regulations.
Modern sampling valve technologies, such as automated systems, increase sampling frequency and reliability, leading to better-informed decision-making and improved resource recovery.
By reducing resource consumption and waste during testing, sampling valves promote sustainability while maintaining high operational standards.
Wenzhou Lifei Stainless Steel Co., Ltd. has over 15 years of experience in manufacturing fluid equipment, focusing on providing innovative and reliable sampling solutions for their customers.
Sampling valves might not be the most glamorous part of industrial equipment, but trust me, they’re pretty essential. They play a big role in making sure everything runs smoothly and that quality control isn't left to chance. When you can take samples quickly and accurately, it’s a game-changer—helps catch issues early, cuts down on waste, and keeps things running efficiently. Take the pharmaceutical world, for example. These valves let folks test products precisely, so that everything stays safe and meets strict standards. It’s all about making sure the final stuff is top-notch.
And it’s not just pharma—these valves are also super important in the oil and gas industries. They help keep safety tight and ensure companies stay compliant with all the regulations. Here at Wenzhou Lifei Stainless Steel Co., Ltd., we totally get how vital reliable fluid equipment like sampling valves is for any industrial setup. With over 15 years of experience in making and exporting these kinds of products, we always put our customers first. Our goal? Help clients succeed with high-quality, tailor-made solutions that fit their specific needs—and maybe make their day a little easier too.